

Intelligent pumping solution
 Leslah Garland 22 October 2026
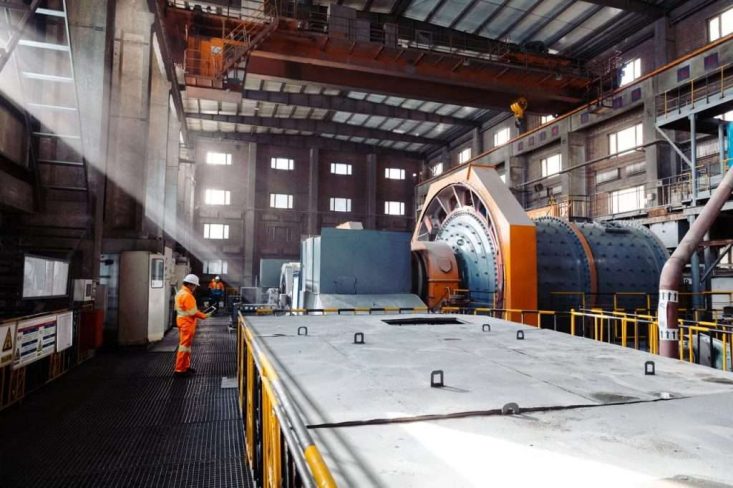
As industrial operations work to control energy consumption as a key component of operating costs, some are finding significant opportunities in the pumping systems behind their specialised equipment. More efficient pumping also lowers the environmental impact of these processes, which is a growing concern for responsible companies, explained Divyanshu Shrivastava, Global Product Manager, Armstrong Fluid Technology – Industrial.
“Rather than assuming that existing equipment is operating as efficiently as possible, operators can examine whether pump selection, system configuration and controls are properly matched to the demands of their application,” said Shrivastava. “In many cases, targeted changes to pumping technology can reduce energy consumption without requiring major changes to the wider infrastructure.”
He pointed to a recent project undertaken with minerals processing specialist Metso Minerals. A review of its high-pressure tube press application led to a new Armstrong Industrial pumping solution that reduced power consumption by 40% – while also lowering service costs and achieving a seven-month payback period.
Ideal match
“Improving pumping efficiency starts with understanding what the application actually requires,” he explained. “Simply replacing an existing pump with a more efficient model may not deliver the optimum result if the pump remains poorly matched to the operating conditions.”
This is particularly important in industrial applications where pumps may need to operate continuously, or meet demanding pressure requirements, he emphasised. The right solution needs to consider factors such as required flow, pressure, duty cycle, reliability, maintenance requirements and the environment in which the equipment operates.
For Metso Minerals, the application involved a tube press system used to remove waste iron and other by-products from furnace exhaust through a variable-volume filtration process. The process applies pressure of up to 100 bar to dewater the slurry and produce a drier filter cake that can be handled, stored or disposed of more easily.
“The existing system used a high-pressure rotary pump driven by a 75 kW motor with low efficiency and a high risk of failure,” he said.
System optimisation
Armstrong Industrial’s replacement solution had to meet demanding operating requirements. The pump unit needed to cycle between load and off-load every five seconds, while the accumulators had to operate within 10% of nominal system pressure, with the option to tighten this to 5%. Above all, the system needed to operate reliably around the clock, 24 hours a day, seven days a week.
“Working together, Metso Minerals and Armstrong Industrial developed a positive-displacement pumping solution comprising S75 Trimax pumps, accumulators and nitrogen-charged back-up bottles,” explained Shrivastava. “Adjustable flow mechanisms and safety devices were incorporated to achieve the required tight hysteresis — the narrow operating range around the system’s pressure set point.”
The key change was therefore not simply a lower-rated motor, but a pumping technology better suited to the application’s demand characteristics, he noted. The positive-displacement system could manage the demand more efficiently, allowing the motor size to be reduced from 75 kW to 45 kW – to achieve the considerable 40% power reduction.
Measurable results
The financial impact of this solution was equally significant. Annual energy costs fell from almost £60,500 with the rotary pump to less than £36,300 with the Armstrong Industrial solution, representing an annual energy saving of over £24,000. A further £7,390 in annual service savings was identified, comprising £5,040 in maintenance time and £2,350 in spare parts.
“The additional installation cost was £19,200, including £18,000 for the pumps and £1,200 for controls,” he said. “Based on the resulting savings, the project could recover its capital costs in just seven months.”
The benefits extended beyond energy consumption, he added. The system incorporated health monitoring, with performance data fed to a remote PLC so engineers could identify and address potential failures before they occurred.
“The pump design was also intended for demanding environments, with enclosed construction helping prevent contaminant ingress and integral water cooling supporting operation in hot or confined spaces,” he said. “Variable speed drive (VSD) technology offered the potential for a further 5-10% power saving.”
Shrivastava concluded that this project demonstrated that improving industrial energy efficiency did not necessarily require major infrastructure changes.
“A targeted assessment of an individual system, supported by appropriate equipment selection, controls and monitoring, can reduce energy consumption and costs while strengthening reliability.

